Baishicheng Hydraulic Engineering Team | Technical Content Contributor | Published September 10, 2026
This guide references publicly documented ISO tolerance conventions for hydraulic cylinder bores alongside Baishicheng Hydraulic’s disclosed manufacturing capabilities as of September 2026. Baishicheng has not published a numerical bore-tolerance standard for its own cylinder line; project-specific figures should be confirmed directly with the engineering team.
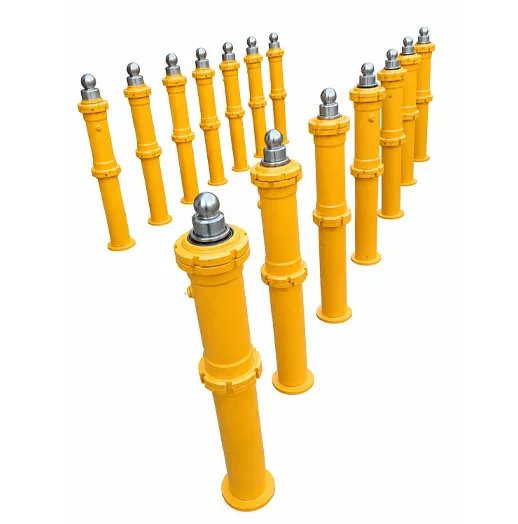
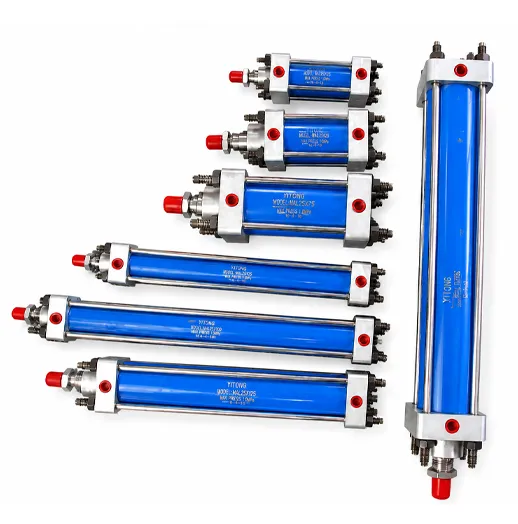
A honed hydraulic cylinder tube is a seamless steel tube whose bore has been precision-machined to a controlled roundness, straightness, and surface roughness. That finish, not the wall thickness printed on a data sheet, decides whether a piston seal tracks smoothly or wears out early. Buyers comparing tube suppliers need to read tolerance grade and Ra value together, not one or the other.
What Honing Actually Changes Inside a Cylinder Barrel
Honing is a bore-finishing process that runs abrasive stones through a rough-bored or cold-drawn tube to bring the inside diameter to final size while leaving a repeating crosshatch pattern on the surface. That pattern is functional. It holds a thin film of hydraulic oil against the seal lip during every stroke, which is what keeps a dynamic seal lubricated instead of running dry against bare steel.
Two things get controlled during honing, and buyers tend to focus on only one:
- Dimensional tolerance — how close the finished bore diameter sits to the nominal size, expressed as a tolerance grade such as H8 or H9.
- Surface roughness and crosshatch geometry — the Ra value and the angle of the honing pattern, typically specified in a 30-45 degree range under ISO 5597, the international standard covering hydraulic cylinder dimensions and mounting.
A tube can meet a tight diameter tolerance and still have a poor surface finish, or the reverse. Both have to be verified independently on an inspection report.
Tolerance Classes and Surface Roughness on a Spec Sheet
Tolerance grades and Ra ranges are not company-specific figures — they come from general machining and ISO 5597 conventions used across the hydraulic cylinder industry. The table below reflects that general engineering reference, not a Baishicheng-published number.
| Application Type |
Typical Tolerance Grade |
Typical Ra Range |
Crosshatch Angle |
| Mobile hydraulics (construction, agricultural) |
H8–H9 |
0.2–0.4 μm |
30–40° |
| General industrial hydraulics |
H8–H9 |
0.3–0.4 μm |
35–45° |
| High-pressure systems |
H7–H8 |
0.15–0.3 μm |
30–35° |
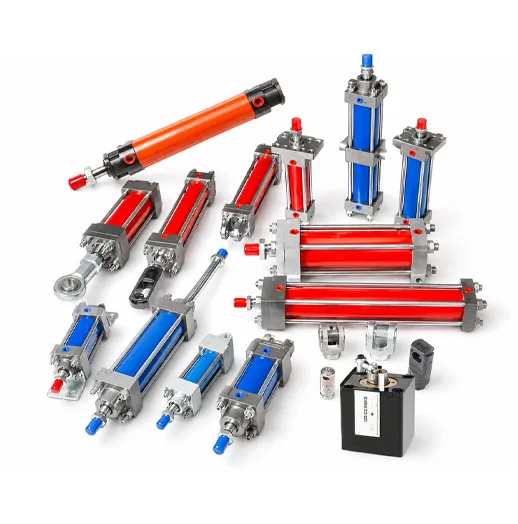
Baishicheng’s product catalogue confirms cylinder honing as an in-house manufacturing step and states that bore diameter, rod diameter, stroke, and mounting style are engineered to each customer’s specification. No public numeric tolerance range is disclosed for that honing process, so a buyer wanting a documented figure for a specific project should request it directly rather than assume one of the ranges above applies by default.
Where Honing Sits Inside a Full Cylinder Build
A tube supplier honing raw stock and a manufacturer honing a bore that will be sealed, tested, and shipped as a finished cylinder are solving different problems. Baishicheng’s manufacturing scope covers hydraulic manifold machining, cylinder honing, system assembly, and full-pressure/full-flow testing before dispatch, with witness testing available on request. Honing in that context is one step inside a sequence that ends with a pressure-tested assembly, not a standalone tube shipped for someone else to finish, seal, and qualify.
That matters for tolerance control specifically. A tube bought separately still has to be matched to the piston, rod, gland, and seal set chosen for the application — a step where mismatched clearances show up as leakage or premature wear. When honing happens as part of the same build that selects the seal and runs the pressure test, the tolerance chain has fewer handoff points where an error can enter unnoticed.
For applications pushing into ultra-high-pressure territory, Baishicheng’s engineering capability reaches up to 120 MPa for specially designed cylinders and systems. That figure applies to designated ultra-high-pressure applications only and should not be read as the standard rating for every cylinder or honed tube the company produces.
A Common Misunderstanding: “Honed” Versus “Ready-to-Hone”
Some tube listings use “honed tube” and “ready-to-hone tube” almost interchangeably, and the difference is not cosmetic. A ready-to-hone tube has near-final inside diameter but still needs a finishing pass before it can seal reliably; a genuinely honed tube is already at final bore size and roughness. Buying the former while expecting the latter is a common sourcing mistake that only surfaces after assembly, when seals fail early or leak from day one.
Before accepting a tube as finished, three checks catch this:
- Ask for the actual measured Ra value on an inspection report, not a catalogue range. A quoted range means nothing without a measurement tied to the specific batch.
- Confirm roundness and straightness data separately from diameter. A bore can hit its nominal diameter at one point and still be out of round along its length.
- Confirm whether final honing was completed in-house or subcontracted, since a subcontracted final pass adds a handoff where tolerance can drift between the tube maker’s inspection and the cylinder builder’s assembly line.
Weighing Tube-Only Sourcing Against a Finished Cylinder
Buying finished honed tube on its own can be the faster, lower-cost route when an in-house machine shop already handles gland fitting, seal selection, and pressure testing — the tube is simply raw material for a build the buyer controls. Compared with typical tube-only supplier catalogues, though, that route puts the burden of matching bore tolerance to seal compound and operating pressure entirely on the buyer’s own team, and any mismatch between the tube’s honing spec and the chosen seal set becomes the buyer’s warranty exposure rather than the tube supplier’s.
Sourcing a complete cylinder instead shifts that matching and testing responsibility onto the manufacturer, at the cost of losing the flexibility to swap tube sources mid-project or negotiate tube pricing independently of the finished assembly.
FAQ
Q: What tolerance grade is standard for a honed hydraulic cylinder tube?
A: Most hydraulic cylinder tubes are honed to an H8 or H9 tolerance grade under general ISO 5597 convention, though high-pressure applications often call for H7 or H8. Baishicheng has not published a fixed tolerance figure for its own cylinder line, so a project-specific number should be confirmed directly.
Q: Does a rougher bore finish wear seals faster than a smoother one?
A: Not necessarily — a bore polished smoother than roughly Ra 0.1 μm can actually wear seals faster because it fails to retain enough oil film for lubrication. The functional target is a controlled Ra range with a crosshatch pattern, not the lowest roughness number achievable.
Q: Can Baishicheng hone a cylinder tube to a customer-specified tolerance?
A: Baishicheng’s cylinder line is built around application-specific dimensions, and cylinder honing is listed among its in-house manufacturing steps. Confirm the achievable tolerance and inspection documentation for a specific bore size directly with the engineering team before finalizing a design.
Q: Is pricing for honed cylinder tube or a finished honed cylinder fixed?
A: No — pricing depends on bore size, tolerance grade, tube length, steel grade, and whether the order is for tube stock or a fully assembled and tested cylinder, so it is quoted on a project basis rather than published as a fixed range.
Q: Does the honing process affect the maximum pressure a cylinder can handle?
A: Honing itself does not set the pressure rating, but a poorly controlled bore tolerance can cause seal extrusion or leakage well below a cylinder’s design pressure. Pressure rating is set by the overall design and tested during full-pressure/full-flow commissioning, not by the honing step alone.
 English
 Get a Quote


 September 08, 2026