Baishicheng Hydraulic Engineering Team | Technical Content Contributor | Published September 2026
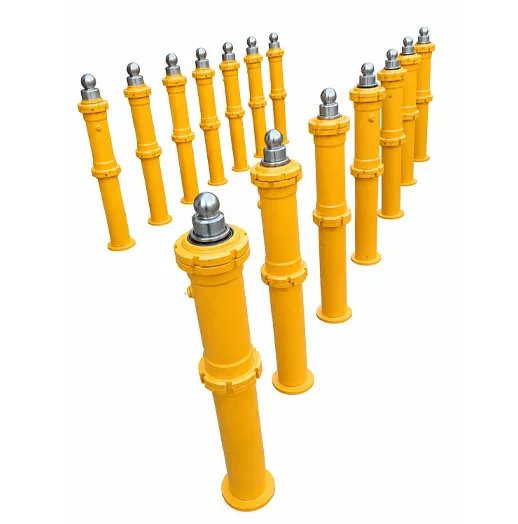
A honed hydraulic cylinder tube is a seamless or welded-drawn steel tube finished internally to a controlled bore diameter and surface texture, typically toleranced to ISO 286 grade H8 or H9, so that piston seals maintain consistent clearance and sealing contact throughout the cylinder’s stroke and service life.
What Honing Does That Standard Steel Tube Cannot
A mother tube — the raw seamless or welded-drawn stock before finishing — comes off the mill with a bore that is round enough for general piping but not round, straight, or smooth enough for a piston seal to run against for years without leaking. Honing corrects that gap. A honing head carries abrasive stones through the bore under controlled pressure, removing a small, even layer of material while a rotating and reciprocating motion cuts a cross-hatch pattern into the surface.
That cross-hatch matters more than most buyers assume. It is not a cosmetic finish. The pattern holds a thin film of hydraulic oil against the bore wall, which lubricates the seal lip on every stroke. A bore that is merely ground or polished smooth can look better under a light but will not hold that oil film the same way, and seal wear shows up faster than the polished appearance suggests. This is a common point of confusion when a buyer compares two tube samples by feel or shine rather than by the actual finishing process used.
How Tight Does the Bore Actually Need to Be?
Tolerance for honed bores follows the ISO 286 hole-tolerance system, most commonly expressed as H7, H8, or H9. The letter identifies the tolerance zone; the number identifies how wide that zone is. A smaller number is the tighter fit — not the looser one, which is a mix-up worth flagging since it runs backward from how some buyers expect grading systems to work.
| Tolerance Class |
Typical Use |
Bore Deviation (100 mm bore, upper limit) |
Common Surface Finish (Ra) |
| H7 |
High-pressure or long-service-life cylinders |
+0.035 mm |
0.2–0.4 µm |
| H8 |
Standard industrial hydraulic cylinders |
+0.054 mm |
0.4–0.8 µm |
| H9 |
General-duty, cost-sensitive builds |
Wider band than H8; exact figure varies by supplier chart |
Typically coarser than H8 |
The deviation figures above scale with bore diameter under ISO 286 — a 50 mm bore and a 200 mm bore in the same class do not carry the same millimeter allowance, so a tolerance chart has to be read at the specific nominal size, not assumed to carry over from a different job.
Surface roughness (Ra) is specified separately from tolerance class, and the two get conflated often enough to cause ordering mistakes. A tube can sit inside an H8 dimensional band and still have a bore finish too coarse or too fine for the seal material planned — polyurethane, NBR, and PTFE composite seals do not all want the same Ra range, so the finish spec should come from the seal supplier’s recommendation, not from habit.
Reading a Honed Tube Order Description
A typical order line reads something like “80 mm ID × 95 mm OD × 1,500 mm long, seamless, H8, Ra ≤ 0.4 µm.” Getting each field right avoids a mismatch discovered only after assembly:
- State the nominal bore ID first, then the OD or wall thickness — wall thickness should be checked against the working pressure with a recognized method rather than copied from a similar job.
- Specify the tolerance class by letter and number (H7, H8, H9) instead of a general phrase like “precision bore,” which has no fixed meaning between suppliers.
- Give the Ra range appropriate to the seal material, not a single target number pulled from an unrelated spec sheet.
- Confirm whether the mother tube is seamless or welded-drawn (DOM). Seamless is generally preferred for high-pressure and fatigue-prone applications; welded-drawn can be a reasonable fit for moderate pressure where cost matters more.
- Request the mill or inspection certificate alongside the tube itself. A tolerance class printed on a quote is not the same as a certificate confirming the specific batch met it.
Where Honing Fits Inside a Full Cylinder Build
Buying honed tube on its own, from a tube-only mill, leaves everything downstream of the bore in someone else’s hands: matching the rod to the honed bore, machining seal grooves, managing weld heat distortion on the end caps, and pressure-testing the finished assembly. Compared with that split-supplier route, an integrated build checks the bore against the completed, pressurized cylinder rather than against the raw tube in isolation.
Cylinder honing is listed among Baishicheng’s disclosed manufacturing steps, alongside hydraulic manifold machining, system assembly, PLC panel integration, full-pressure and full-flow testing, and pre-shipment commissioning, with factory witness testing available on request. The company’s custom cylinder lines — including Custom Hydraulic Cylinders, Stainless Steel Hydraulic
Cylinders, and the HOB, MOB, and MOB Front Flange series — are engineered around each project’s bore diameter, rod diameter, stroke, load, mounting style, and operating pressure rather than a fixed catalog range. Baishicheng does not publish a standard numerical range for these dimensions; buyers working to a specific tolerance chart or bore size should confirm the figure directly for their application rather than assume a published default exists.
For applications rated well above conventional hydraulic pressure, Baishicheng also states design and manufacturing capability up to 120 MPa. That figure applies to specially engineered systems and cylinders built for designated ultra-high-pressure applications — it is not the working pressure of a standard honed cylinder tube order, and it should not be read as such.
Where a Standard Honed Bore Falls Short
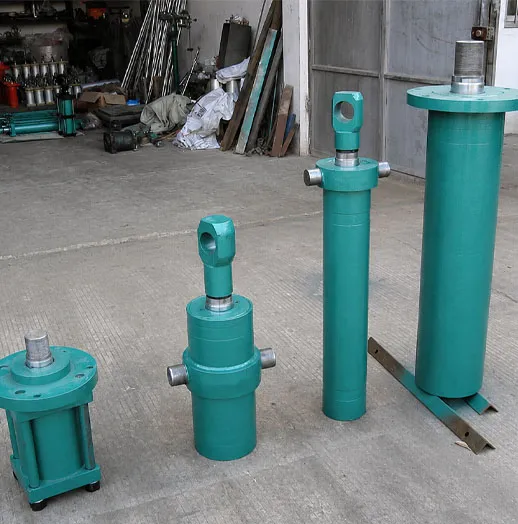
Not every application should default to a mid-range H8 finish. Mobile equipment with high cycle counts, marine or washdown environments, and cylinders running above roughly 250–300 bar tend to push toward H7 tolerance and the tighter end of the Ra range, since a slightly loose fit that is invisible in a low-cycle industrial press shows up as internal leakage or accelerated seal wear much sooner under continuous duty. On the other end, specifying H7 and a fine Ra finish for a low-cycle, low-pressure application adds cost without a matching gain in service life — the tolerance class is a decision tied to duty cycle and pressure, not a default “tighter is always better” choice.
FAQ
What does “honed” mean for a hydraulic cylinder tube?
Honing is a precision internal-bore finishing process that removes a controlled layer of material and cuts a cross-hatch pattern into the surface, producing the roundness, straightness, and oil-retaining texture a piston seal needs to run against reliably.
What is the practical difference between H8 and H9 tolerance?
H8 holds a tighter bore-diameter allowance than H9 at the same nominal size, and H8 is the more common default for standard industrial hydraulic cylinders; H9 is generally reserved for general-duty builds where cost outweighs the need for the tighter fit.
Can both seamless and welded-drawn tube be honed to the same tolerance class?
Yes, tolerance class is a finishing specification applied after the mother tube is selected, though seamless tube is typically favored for high-pressure or fatigue-critical applications while welded-drawn tube suits moderate-pressure, cost-sensitive builds.
How do I know what surface roughness (Ra) my cylinder needs?
Surface roughness should be set according to the seal material specified for the cylinder, since NBR, polyurethane, and PTFE composite seals do not perform identically against the same Ra finish, and the seal supplier’s recommendation is the more reliable source than a generic target figure.
Does Baishicheng manufacture honed cylinder tube in-house?
Cylinder honing is listed among Baishicheng’s disclosed in-house manufacturing steps and is applied as part of building complete custom hydraulic cylinders; the sourcing of raw mother tube stock prior to honing is not detailed publicly, so buyers with a specific mother-tube-source requirement should confirm it directly when requesting a quote.
 English
 Get a Quote


 September 01, 2026